1. Sink Marks
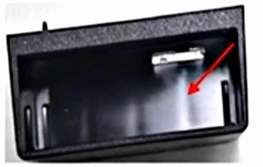
Symptom: The outer wall of the part caves inward; crescent-shaped depressions appear on the surface opposite ribs or bosses.
Corrective Actions:
- Optimize wall thickness for uniformity; core out thick sections to eliminate heavy mass areas.
- Increase packing (hold) pressure and extend packing time.
- Enlarge the gate and increase runner cross-section to prevent premature gate freeze-off.
- Reduce melt temperature and lower mold temperature.
2. Bubbles / Vacuum Voids
Symptom: Circular cavities visible in cross-section. Gas bubbles tend to occur near the surface, while vacuum voids form at the center of thick wall sections.
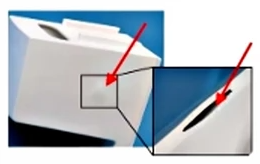
Corrective Actions:
- Reduce thick wall sections where possible.
- Ensure thorough pre-drying of raw material (resin).
- Increase packing pressure and extend packing time.
- Optimize venting grooves; improve mold venting.
- Moderately reduce injection speed to minimize air entrapment.
3. Flash (Burr)
Symptom: Thin excess plastic fins at the parting line, around inserts, or at ejector pin locations.
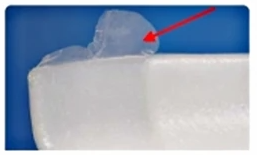
Corrective Actions:
- Increase clamping force.
- Lower melt temperature and mold temperature to reduce melt fluidity.
- Reduce injection pressure and packing pressure; apply a stepped pressure reduction profile.
- Re-spot (blue-match) and repair the parting line surface; tighten insert fit clearances.
4. Weld Lines (Knit Lines / Meld Lines)
Symptom: A visible fine line appears where two melt flow fronts converge and merge.
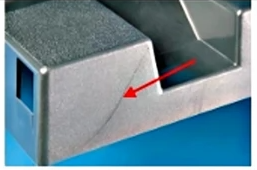
Corrective Actions:
Minimize holes/core-outs in the part design; relocate gates so that weld lines fall away from cosmetic surfaces.
Add venting grooves at the weld line location; increase vent depth/area.
Raise melt temperature and mold temperature.
Moderately increase injection speed to keep the flow fronts hot at the point of convergence.
5. Silver Streaks (Splay Marks / Moisture Streaks)
Symptom: Silvery-white, streak-like lines on the part surface, oriented along the melt flow direction.
Corrective Actions:
Strictly enforce proper resin drying procedures (time, temperature, dew point).
Lower barrel zone temperatures to prevent thermal degradation of the material.
Moderately increase screw back pressure to expel entrapped gases and volatiles from the melt.
6. Warpage (Distortion)
Symptom: The part bows, twists, or exhibits out-of-flat surfaces after cooling and ejection.
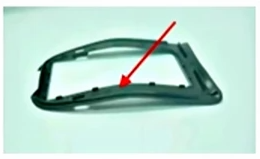
Corrective Actions:
- Design for uniform wall thickness; maintain symmetrical geometry wherever possible.
- Adjust cooling channel layout to balance temperatures between the cavity (A-side) and core (B-side).
- Use balanced multi-gate feeding; optimize the packing pressure profile.
- Revise ejector pin layout to ensure simultaneous, uniform ejection.
7. Short Shot (Incomplete Fill)
Symptom: Localized areas of the part remain unfilled — typically at corners, edges, or thin-wall sections.
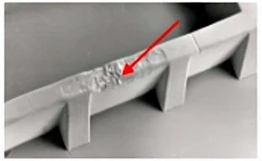
Corrective Actions:
- Increase injection pressure and boost fill speed.
- Raise melt temperature and mold temperature to reduce viscosity.
- Enlarge runner and gate dimensions.
- Widen and deepen parting-line vents to improve air evacuation.
8. Ejector Pin Stress Whitening (Ejector Marks / Stress Blush)
Symptom: A whitened ring or halo appears on the part surface directly opposite the ejector pin contact area.
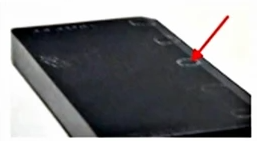
Corrective Actions:
- Increase draft angles on both internal and external part surfaces.
- Add more ejector pins to distribute ejection force over a larger area.
- Polish the cavity surface to reduce demolding friction and release resistance.
For more frequently asked questions, please click the link below.
This article summarizes 27 common defects in injection molding production, covering their definitions, causes, and targeted solutions. The content is precise and practical, suitable for direct reference in production debugging.
 Consumer electronics HOTFrom prototype to production to homes around the world
 Automotive HOTDrive product development and speed up innovation
 Medical NEWAccelerating new product introduction for the medical industry
 Robotics & automation NEWBuild the most complex automated systems with ease
 Industrial machineryPower your machines with cutting-edge technologies