Help Center
Deliver to:
Ship to
Currency
USD (US Dollar)
Save
Your Cart
Your quote requests is empty.
Welcome back! If you had Quote requests items in your Shopping cart, we have saved them for you. You can Sign in now to see them, or whenever you're ready to check out.
Total $0.00
View Cart
Start A New CNC Quote
STEP | STP | X_T | IGES | IGS | SLDPRT files
All uploads are secure and confidential
Capabilities
Advantages
Materials
Finishes
Resources
Quote Now!
Overview
Our EDM Service
What is Electrical Discharge Machining (EDM)
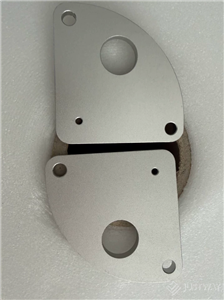
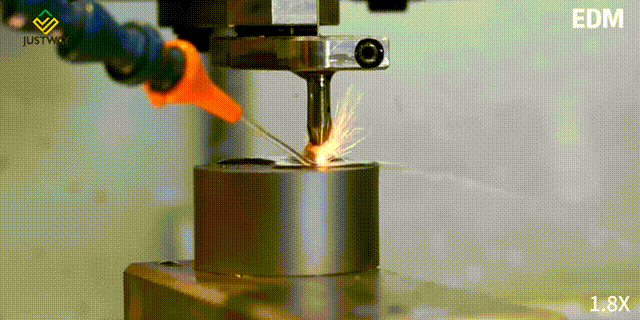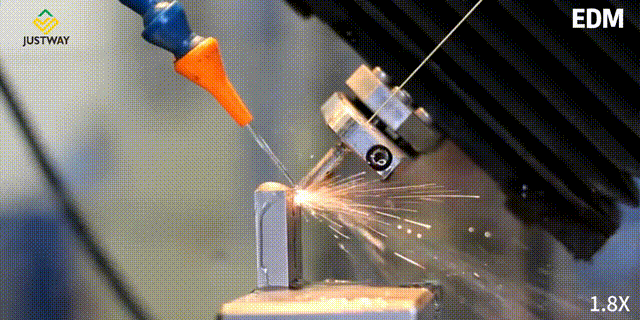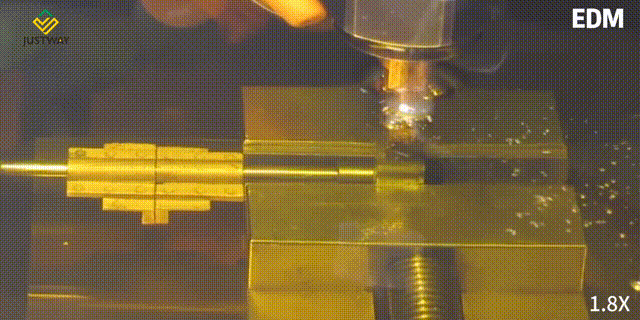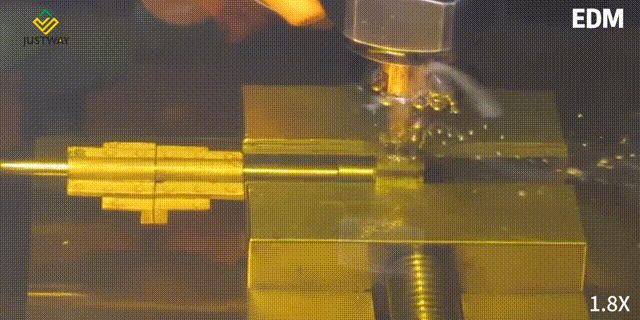
EDM is a special processing method that uses the electric erosion effect generated by the pulse discharge between the two electrodes immersed in the working fluid to remove conductive materials.
CNC Electrical Discharge Machining gif Video
How Does EDM Work?

During EDM, the tool electrode and the workpiece are respectively connected to the two poles of the pulse power supply, and immersed in the working fluid, or the working fluid is filled into the discharge gap. The tool electrode is controlled to feed to the workpiece through the gap automatic control system. When the gap between the two electrodes reaches a certain distance, the pulse voltage applied to the two electrodes will break down the working fluid and generate spark discharge. A large amount of heat energy is concentrated instantaneously in the tiny channel of discharge, the temperature can be as high as 10,000 degrees Celsius, and the pressure also changes sharply, so that a small amount of metal material on the working surface immediately melts and gasifies, and splashes into the working fluid in an explosive manner In the process, it condenses rapidly to form solid metal particles, which are taken away by the working fluid.
At this time, a tiny pit trace is left on the surface of the workpiece, the discharge pauses for a short time, and the working fluid between the two electrodes returns to the insulating state. Immediately afterwards, the next pulse voltage breaks down at another point where the two electrodes are relatively close to each other, generating spark discharge, and repeating the above process. In this way, although the amount of metal removed by each pulse discharge is very small, because there are tens of thousands of pulse discharges per second, more metal can be removed, which has a certain productivity. Under the condition of maintaining a constant discharge gap between the tool electrode and the workpiece, while removing the metal of the workpiece, the tool electrode is continuously fed to the workpiece, and finally the shape corresponding to the shape of the tool electrode is processed. Therefore, as long as the shape of the tool electrode and the relative motion between the tool electrode and the workpiece are changed, various complex profiles can be processed.
Tool electrodes are usually made of electro-corrosion-resistant materials with good conductivity, high melting point and easy processing, such as copper, graphite, copper-tungsten alloy and molybdenum. During the machining process, the tool electrode also has loss, but it is less than the erosion amount of the workpiece metal, and even close to no loss. As the discharge medium, the working fluid also plays the role of cooling and chip removal during the machining process. Commonly used working fluids are media with low viscosity, high flash point and stable performance, such as kerosene, deionized water and emulsion. EDM mainly includes two process methods of electric discharge forming and electric discharge wire cutting.

Other Benefits of EDM
The cutting speed is fast, which can realize fast machining, especially for hard metal materials. High processing precision, EDM can provide fine and smooth surface quality. The cutting depth is controllable, and the cutting depth can be adjusted according to the characteristics of the workpiece. It has a wide range of applications and can be used to process various metal and non-metal materials.
In general, EDM is an efficient and precise cutting process suitable for machining various metals. But at the same time, safety measures need to be taken to prevent harm to the human body.
Features of EDM
Advantages
Wide range of applications
It can be processed regardless of the thickness and hardness of the material. As long as it is a conductive material, it can be processed from a thin plate to a cemented carbide, regardless of the thickness, size and hardness of the material.
Complicated shapes can be processed
In addition to straight cutting, it is also possible to cut into arcs and process complex shapes, such as a combination of straight lines and arcs. Taper processing is also possible by moving the upper and lower wires separately.
High precision
The accuracy of wire cutting is comparable to that of a grinder (0.005 mm unit).
Reduce material damage
Since wire cutting is a non-contact process, the load on the material is not too great and the thermal deformation is minimal.
Drawbacks
Bottom processing is not possible
Since wire cutting is a wire saw, it cannot be processed with the bottom. If you want to EDM the bottom, then a sinker EDM is the best choice.
Slow processing
It cuts while gradually melting the workpiece, so it works slower than cutting and is not suitable for mass production. Its speed is a few millimeters per minute, and it is barely visible to move with the naked eye.
Non-conductive materials cannot be handled
While conductive materials can be processed regardless of their hardness, non-conductive materials cannot.
Custom Material
The materials available on the online system may not be exhaustive of all materials available on the market. If the materials you need are not listed on the order page, please select "custom" under the material menu, and our engineers will review and purchase.
Our standard surface finishes
FAQ's
What is CNC machining?

CNC machining is a modern manufacturing technique that utilizes programmable software and computer-controlled equipment to create complex parts and products from a wide range of materials such as metal, plastics, and wood.

With CNC (Computer Numerical Control) technology, the manufacturing process is highly automated and precise. The process begins with a CAD (Computer-Aided Design) file, which is converted into a set of instructions in the form of G-code. This code is then sent to a CNC machine, which follows step-by-step instructions to produce the desired part or product.

CNC machining has revolutionized the manufacturing industry by increasing productivity, improving accuracy, reducing waste, and allowing for complex shapes and designs to be produced with high precision. It is used in a variety of industries, including aerospace, automotive, electronics, and medical devices.

The following link is the detailed content suitable for professional machining engineers to view

>>The Ultimate Guide to CNC Machining: How It Works, Types, and Applications

What are the benefits of using CNC machines?

The benefits of using CNC machines are:

1. Enhanced precision: CNC machines can produce highly precise and accurate parts with tolerances as low as 0.0002 inches, which is not possible manually.

2. Increased speed: CNC machines are automated and can run 24/7, thereby offering faster production time for large volumes of parts.

3. Consistency: Unlike manual production, CNC machines produce parts that are identical in terms of size, shape, and quality consistently.

4. Reduced labor costs: CNC machines require less manual labor and supervision, which saves labor costs and improves overall efficiency.

5. Flexibility: CNC machines can be reprogrammed easily to create different parts without the need for complex tool changes.

6. Ability to work with a wide range of materials: CNC machines can work with a variety of materials, including metals, plastics, wood, and composites.

7. Improved safety: CNC machines can run automatically, which reduces the risk of injury for workers and provides a safer work environment.

8. Reduced waste: The precision offered by CNC machines reduces the material waste and scraps generated during the production process.


What types of materials can be used with CNC machines?

CNC machines can work with a wide range of materials including metals, plastics, wood, composites, ceramics and more. The types of materials that CNC machines can work with depend on the specific capabilities of the machine, the tooling options available, and the type of work being performed. Here are some examples of materials that can be used with CNC machines:

1. Metals: CNC machines can work with a variety of metals, including steel, aluminum, brass, titanium, copper, and more.

2. Plastics: CNC machines can work with various types of plastics such as polycarbonate, acrylic, nylon, ABS, PVC, and more.

3. Wood: CNC machines also perform operations on hardwood, softwood, plywood, and MDF board.

4. Composites: CNC machines can work with glass and carbon fiber composites, Kevlar, and other composite materials.

5. Ceramics: Machinable ceramics can also be used with CNC machines like porcelain, alumina, zirconia and other materials.

It's important to note that different CNC machines will have specific requirements for the materials that can be used. The feed rate, chip load, and spindle speed will vary depending on the material, so it's essential to understand the material properties and choose the appropriate tools and settings for each job.


What is the difference between CNC milling and CNC turning?

CNC turning and CNC milling are both processes used in CNC machining, but there are some significant differences between the two.

1. Operation: In CNC turning, a stationary cutting tool is used to remove material from a rotating workpiece, whereas in CNC milling, the cutting tools rotate and move across the stationary workpiece.

2. Geometry: CNC turning is more suitable for creating cylindrical shapes such as bolts, nuts, pipes, and shafts. CNC milling is better suited for more complex geometries such as pockets, slots, and complex shapes.

3. Tooling: Turning tools are generally simpler and more robust, while milling tools are more complex and can have more cutting edges.

4. Materials: CNC turning machines are mostly used for turning materials such as round bars, billets, and blocks, while CNC milling machines are used for a wide range of materials such as metals, plastics, wood, and composites.

5. Speed: In general, CNC turning is faster than CNC milling, as the tools are shorter and the process is simpler.

6. Cost: CNC turning is usually less expensive than CNC milling, as the tools are simpler and less expensive.

In summary, CNC turning is best suited for creating simple cylindrical shapes, while CNC milling is better suited for creating more complex geometries. Both processes have their advantages, and the choice between them will depend on the specific requirements of each job.


What is the maximum size of parts that can be machined with CNC machines?

The maximum size of parts that can be machined with CNC machines depends on the size and capacity of the machine being used. CNC machines come in various sizes, and they have different work envelopes that dictate the maximum size of parts they can handle.

Small CNC machines are ideal for small and intricate parts, while larger machines are used for bigger parts. Generally, the maximum size of parts that can be machined on a CNC machine ranges from a few centimeters to several meters.

For example, a small benchtop CNC milling machine may have a work envelope of around 300mm x 300mm x 200mm, while a larger vertical machining center may have a work envelope of 2000mm x 1000mm x 1000mm. In comparison, large gantry-style CNC machines used in the aerospace industry have a work envelope of over 30 meters in length.

It's essential to consider the size and weight of the parts being machined and the capabilities of the CNC machine when selecting a machine for a specific job.


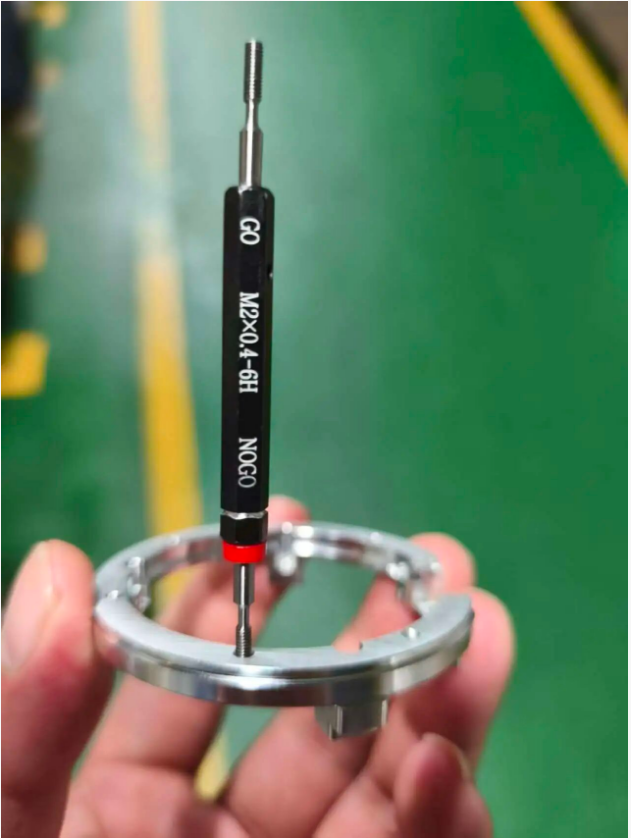
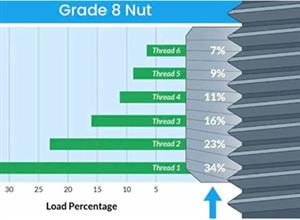
Thread No-Go Gauge Over-Screwing Rectification Procedure

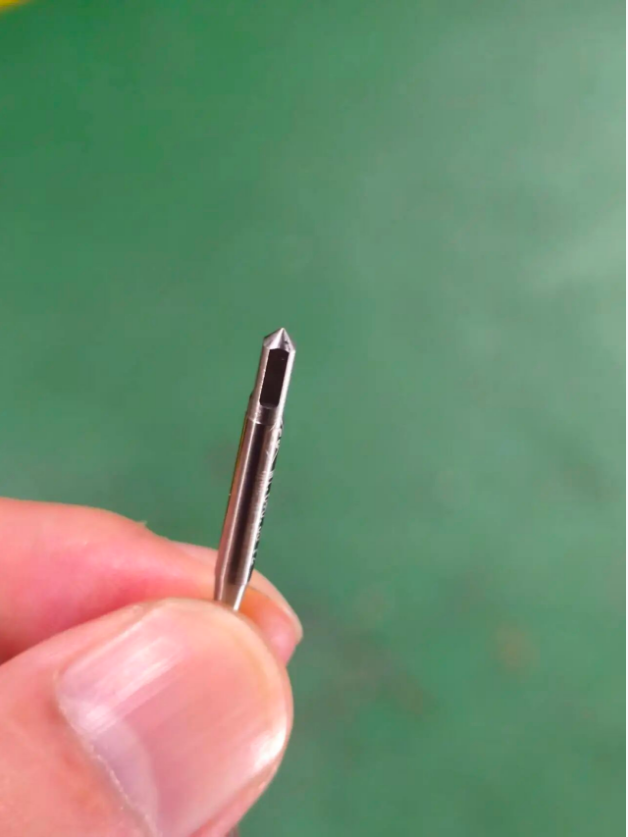
Tool Preparation: Get a used tap shank or center punch.

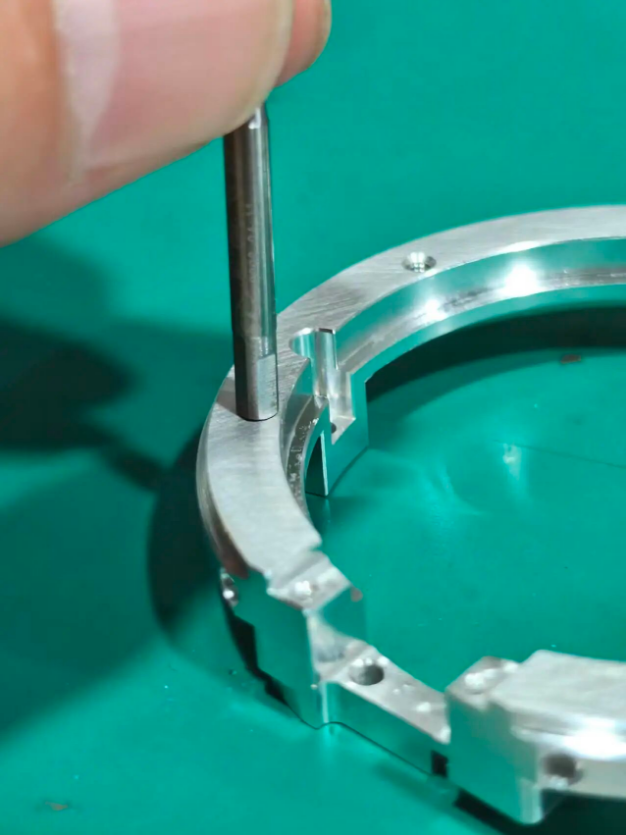
  1. Correction & Repair: Align the rear end of the tap vertically with the threaded hole, then gently tap to correct the thread form.
  2. Re-inspection & Verification: Check with the thread go/no-go gauge. Confirm the go gauge fits properly and the no-go gauge meets specification. Repeat Step 2 if the result fails inspection.
  3. Non-Conforming Disposition: Place permanently defective parts in the designated non-conforming area and scrap bin.

Supplementary Instructions

  • Principle: Gentle tapping corrects minor issues including distorted thread profiles, pitch errors and hole misalignment. This method only applies to slight no-go gauge deviations. Severely damaged threads shall be scrapped directly without forced rework.
  • Tapping Force Requirement: Use light tapping force to prevent secondary damage to the thread substrate and further thread form / bore distortion.
  • Acceptance Criterion: Only parts that fully pass the thread gauge inspection can proceed to the next process. Non-conforming products must never flow downstream.
What are the applications of CNC machining?

Thanks to its high precision, efficiency, and flexibility, CNC machining is widely used across various sectors of modern manufacturing. Here are the main industries and specific application scenarios:

1. Automotive & New Energy Vehicles (NEV)

Core Components: Engine blocks, cylinder heads, crankshafts, camshafts, transmission gears, and chassis suspension parts. These require extreme precision, which CNC machines achieve through complex surface machining.

NEV Parts: Motor housings, battery pack structural components, reducer housings, and molds for silicon carbide (SiC) power devices, catering to the rapid iteration and flexible production needs of the NEV sector.

2. Aerospace & Defense

Complex Surfaces: Aircraft fuselage frames, landing gear, engine blades, impellers, and blisks (bladed disks). These often require 5-axis simultaneous CNC milling for complex geometries.

Hard-to-Machine Materials: Precision machining of difficult-to-cut materials like titanium alloys and superalloys to meet lightweight and strength requirements for aircraft.

Defense Equipment: Tank gun barrels, missile bodies, and radar structural components, meeting strict tolerances and complex contour requirements.

Note: Justway does not manufacture nor accept orders for military weapons, missiles, military drones, or related products.

3. Mold & Die Manufacturing (The "Mother of Industry")

Cavity & Surface Machining: Machining of cavities and cores for injection molds, stamping dies, and die-casting molds. This is often combined with EDM (Electrical Discharge Machining) and wire cutting to ensure high precision and surface quality.

4. Electronics & Consumer Electronics (3C)

Precision Parts: Metal phone bezels, laptop heat sinks, computer casings, camera brackets, internal connectors, and PCBs. CNC machining meets the demand for thinner, lighter designs with tight tolerances, adapting to the fast-paced iteration of consumer electronics.

5. Medical Devices

Implants & Instruments: Artificial joints, orthopedic implants, dental implants, surgical instruments, and medical equipment housings. These require extreme precision, surface finish, and biocompatibility, which CNC machines can achieve on complex curved surfaces.

6. General Machinery & Construction Equipment

Basic Components: Gears, bearings, shafts, discs, pumps, valves, hydraulic components, and boxes/pins for construction machinery (e.g., excavators, loaders). CNC machines replace conventional to improve efficiency and precision while reducing human error.

7. New Energy & Power Equipment

Large-Scale Components: Wind turbine main shafts, gearbox parts, photovoltaic silicon wafer cutting equipment components, and energy storage cabinet structures. Large CNC machines (such as gantry machining centers) handle high-precision machining of large-sized components.

8. Shipbuilding

Large Structures: Hull plates, large propellers, and marine diesel engine components. Large CNC equipment is used to ensure high-precision machining of massive parts, guaranteeing vessel performance.

9. Other Fields

Rail Transit: Precision machining of high-speed rail bogies, axles, and braking system components.

Light Industry & Home Appliances: Machining of molds for appliance casings and consumer electronics shells.

R&D & Repair: Used alongside 3D printing for part repair, small-batch prototyping, and component machining in scientific research and experiments.

By using programmed control, CNC machining can quickly switch production tasks, adapting to multi-variety, small-batch, and complex-shaped manufacturing needs. It has become a core technology in modern high-end manufacturing.

What are the advantages and disadvantages of CNC machining?

As a core technology in modern manufacturing, CNC machining offers significant advantages such as high precision, high efficiency, and strong adaptability. However, it also has limitations, including high initial investment and demanding programming requirements. The specific pros and cons are as follows:

I. Advantages of CNC Machining

High Precision and Consistent Quality: CNC machines are controlled by computer programs, eliminating human error. Precision can reach the micron level with extremely high repeatability, ensuring consistency across large batches of parts. This is particularly suitable for high-precision industries such as aerospace and medical devices.

High Production Efficiency: With a high degree of automation, CNC machines can run continuously. Combined with automatic tool changers (ATC), they significantly reduce setup, tool setting, and auxiliary time. Machining speeds are far faster than traditional manual machining, making them ideal for mass production.

Strong Adaptability and Flexibility: Different parts can be machined quickly by simply modifying the machining program, without the need for frequent changes of complex fixtures. This is well-suited for high-mix, low-volume production, new product development (NPD), and the machining of complex surfaces.

Strong Capability for Complex Geometries: CNC machines (such as multi-axis simultaneous machines) can machine complex profiles, spatial surfaces, and fine details that are difficult or impossible to achieve with conventional machine tools, offering a wide machining range.

Reduced Labor Costs and Workload: Automated machining reduces dependence on highly skilled manual machinists. One operator can run multiple machines simultaneously, lowering labor costs. Additionally, operators stay away from the machining area, improving safety.

Reduced Material Waste: By precisely controlling toolpaths and cutting parameters, material waste can be minimized, reducing the per-part machining cost (when reaching economic batch sizes).

II. Disadvantages of CNC Machining

High Initial Investment: The acquisition cost of CNC machines, supporting CAD/CAM software, high-precision cutting tools, and fixtures is relatively high, posing a significant financial barrier for small and medium-sized enterprises (SMEs).

Complex Programming and Setup: Professional programmers are required to write machining programs. Programming for complex parts is time-consuming and demands high technical expertise. Upfront programming and program debugging add time and cost.

High Maintenance and Repair Costs: CNC machines have complex structures and have strict requirements for the working environment (e.g., constant temperature and humidity) and power supply stability. Repairs require specialized technicians, resulting in higher maintenance costs.

Not Ideal for Very Low-Volume / Single-Piece Production: Due to the time required for upfront programming and machine setup, the overall cost for very small batches or single-piece production may be higher than traditional manual machining, making it less cost-effective.

High Demand for Operator Skills: Although pure manual operation is reduced, operators are required to possess comprehensive skills in machining, programming, and CNC system operation, leading to higher personnel training costs.

What Tolerances Can CNC Machining Achieve?

CNC machining can achieve a wide range of tolerances, from conventional ±0.1 mm to precision levels of ±0.01 mm. The achievable accuracy is not determined by a single factor; it depends on the combined effect of part geometry, material, process planning, machine condition, and inspection methods.

Typical Tolerance Ranges

Conventional Machining: ±0.05 mm to ±0.1 mm. Suitable for most general mechanical structural parts, housings, brackets, and similar components (supported by Justway).

Precision Machining: ±0.01 mm to ±0.02 mm. Common for automotive components, precision molds, and robotic structural parts (supported by Justway).

Ultra-Precision Machining: ±0.001 mm to ±0.005 mm. Typically required for critical aerospace components, medical implants, and optical instruments (currently not supported by Justway).

Key Influencing Factors

Machine Tools and Process Planning: Five-axis machines are better suited for complex surfaces and can reduce setup errors caused by multiple clamping operations. However, three-axis machines with dedicated fixtures may deliver more stable results for simpler geometries. Separating roughing and finishing operations is critical for stress relief and dimensional stability.

Material and Fixturing: A material’s thermal expansion coefficient and internal stress can affect dimensional stability. Improper fixturing that causes deformation or vibration is one of the main reasons for out-of-tolerance results.

Environment and Inspection: A temperature-controlled workshop, such as 20°C ±0.5°C, is essential for maintaining micron-level accuracy. Final accuracy should be verified with precision inspection equipment such as a CMM, rather than relying solely on the machine tool’s nominal accuracy.

Practical Recommendations

Apply Tolerances Reasonably: Specify tight tolerances only on mating surfaces, sealing surfaces, and locating features. Non-critical dimensions should be relaxed to help control cost.

Clarify Inspection Requirements: State inspection methods and applicable standards on the drawing, such as ISO 2768-m or GD&T geometric tolerances, to avoid disputes during delivery.

Provide Complete Information: Supply Justway with 3D models, 2D drawings, material specifications, intended application, and key functional requirements. This helps generate a more accurate process plan and tolerance commitment.

How much does your CNC machining service cost?

CNC machining does not have a uniform fixed price; the final cost is calculated based on a comprehensive assessment of your specific machining requirements. The core pricing logic is:

(Machine Hourly Rate + Material Cost + Programming / Setup / Inspection and Other Surcharges / Order Quantity)

1. Machine Hourly Rate (Core Cost)

Billing Method: Charged based on actual machine machining time (per hour), typically including machine depreciation, electricity, labor, and base profit margin.

2. Material Cost

Billing Method: Based on the actual weight or volume of raw material consumed by the part, considering material utilization rate (waste from cutting solid blocks).

3. Programming and Setup Fees (Fixed Cost)

Billing Method: For single-piece or small-batch orders, the fixed costs of programming and setup/debugging need to be allocated. Complex parts require more programming time and cost more; large batch orders can spread this cost, and some factories include it in the hourly rate.

4. Additional and Hidden Costs

Tool Wear: Complex parts require multiple tools, and tool wear is allocated to the per-part cost.

Inspection Fees: High-precision parts require coordinate measuring machines and other inspection equipment; some factories charge separately.

Post-Processing Fees: Deburring, surface treatment (such as sandblasting, anodizing); some factories charge separately, while others bundle it into the machining cost.

5. Order Quantity (Economies of Scale)

Single-Piece / Small Batch: Fixed costs (programming, setup) cannot be spread out, resulting in higher per-part quotes (e.g., single-piece quotes may reach hundreds of yuan).

Large Batch (e.g., hundreds of pieces or more): Fixed costs are significantly spread out, and per-part quotes drop considerably (e.g., per-part quotes may drop to just a few dollars).

Cost Estimation Advice

When requesting a quote, we recommend providing Justway with complete CAD drawings and technical requirements, and asking for a detailed itemized quotation (clearly separating hourly rates, materials, programming, post-processing, etc.) for accurate price comparison.

For simple plate parts, material costs may be the largest component. But for complex cavities or thin-wall parts, the majority of the cost is in machine time and programming.

Material Cost: Typically 10% to 40% of total cost. The more expensive the material and the larger the difference between blank size and finished part, the higher the waste.

Programming Fee: 5% to 25% of total cost. The more complex the surfaces and the more axes required, the more challenging the toolpath planning.

Machine Hourly Rate: 30% to 70% of total cost — often the largest single component. This includes cutting time, tool changes, flip-and-setup time, etc.

Other Costs: Tooling/inspection and surface treatment each account for 5% to 25%. If you need a CMM report or anodizing, those are billed separately.

For the most accurate quote, provide all drawings, quantities, and any special inspection requirements upfront. Justway has an online pricing system and professional engineers who can quickly deliver precise quotes.

Detail:How CNC Machining Costs Are Calculated: A Complete Cost Breakdown