For the material grade C3604BD with outer diameter ∅79, dimensional deformation was observed during machining. In contrast, production using the outer diameter ∅80 specification was normal. Corresponding analysis was conducted after sampling, and the results are as follows:
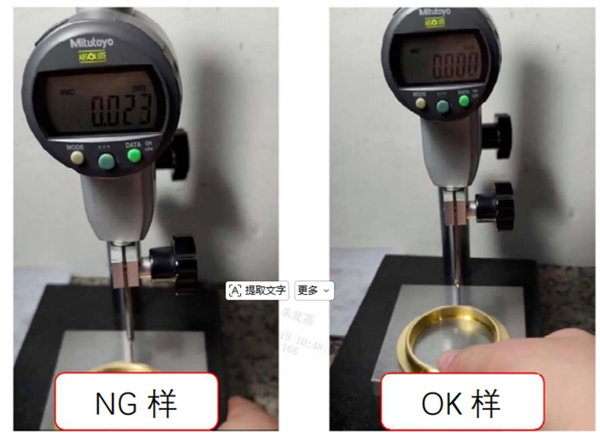
As shown in the defect images, compared with the OK sample, the NG sample exhibits a deformation issue at the edge.
Copper Alloy Chemical Composition Analysis (ICP) GB/T 5121.27-2008 ICP Spectrometer T300110
Determination of Copper Content in Brass (Titration) YS/T910-2013 Buret Setup B300018
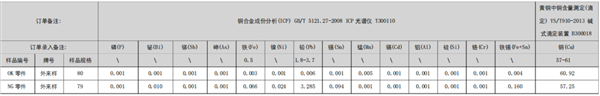
Conclusion: The chemical composition of the NG part complies with the national standard requirements for C3604BD.
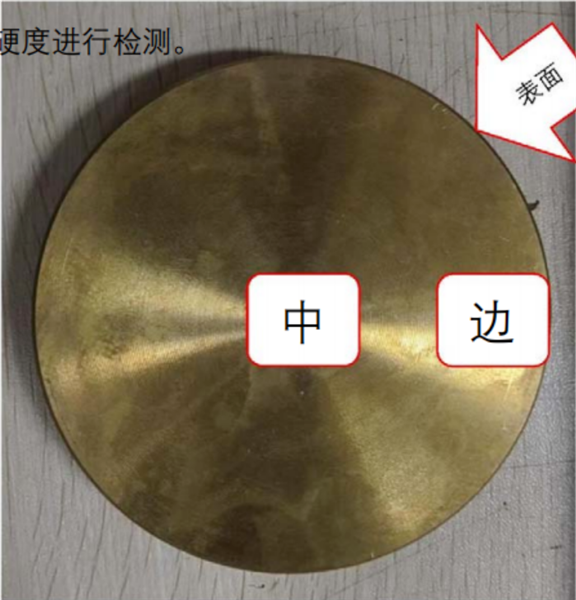
Hardness measurements were performed on the center cross-section, edge cross-section, and surface of the material.
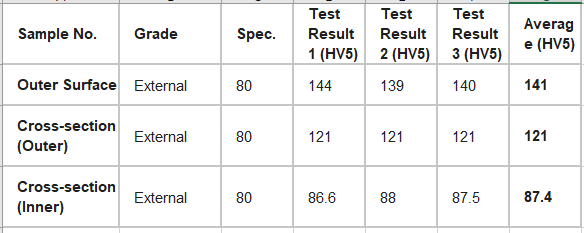
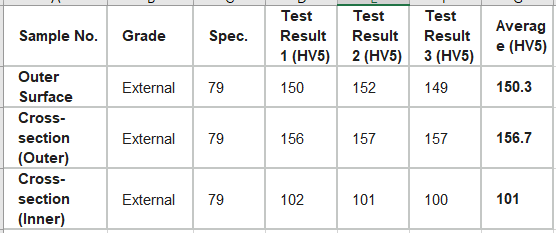
Summary: The overall hardness of the ∅79 specification material is higher than that of the ∅80 specification. Furthermore, the hardness difference between the central cross-section and the outer region is larger (55.7 HV for ∅79 vs. 33.6 HV for ∅80).
Compare the external metallography with the internal metallography
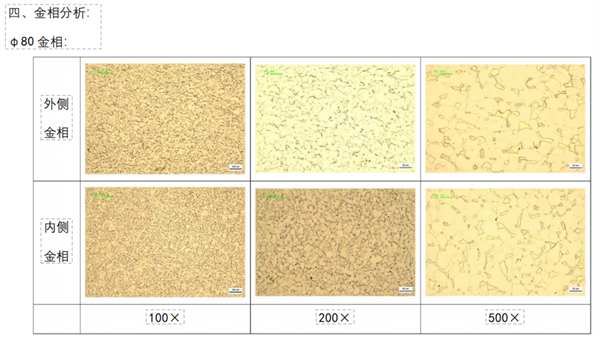
Compare the external metallography with the internal metallography
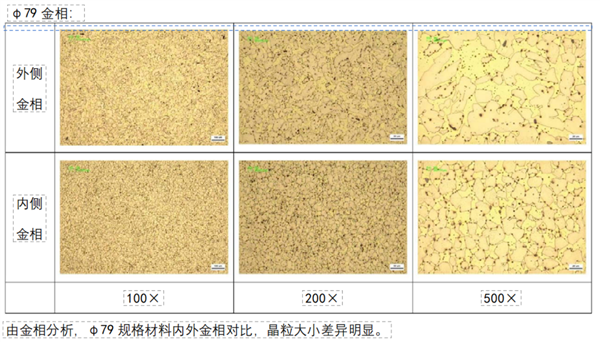
Summary: Metallographic analysis shows a clear difference in grain size between the inner and outer microstructures of the ∅79 specification material.
Based on the above analysis, the significant difference in internal and external hardness of the ∅79 part is the direct cause of stress deformation during machining.
Melting -> Extrusion -> Direct Drawing -> Sizing -> Annealing (Red) -> Inspection -> Packaging
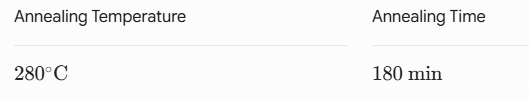
Investigating the production line revealed that our company used low-temperature annealing parameters (280°C / 180min) during the annealing process. Insufficient annealing temperature and duration are the root causes leading to the microstructural grain variance between the interior and exterior of the material.