Author: Machining & Quality Engineer @ Justway
Category: CNC Machining / Process Optimization / Quality Engineering
During quality inspection of a precision machined aluminum housing component, thread inspection failed to meet acceptance criteria using a standard Thread Go-Gauge (通规). The Go-gauge stopped prematurely or felt excessively tight in multiple workpieces.
Through systematic root cause analysis, our engineering team identified multiple contributing factors across machining, post-processing, and surface coating operations. By implementing targeted corrective actions, we resolved the issue completely, achieving a 100% thread acceptance rate in serial production.
During inspection, several internal threaded holes failed the Go-gauge test. Further investigation revealed three primary defect modes:
Testing soft aluminum threads with standard steel gauges before anodizing led to minor local indentations and damage on the thread flanks, causing the Go-gauge to bind or stop.
📍 [Thread Damage / 螺纹氧化前损伤]
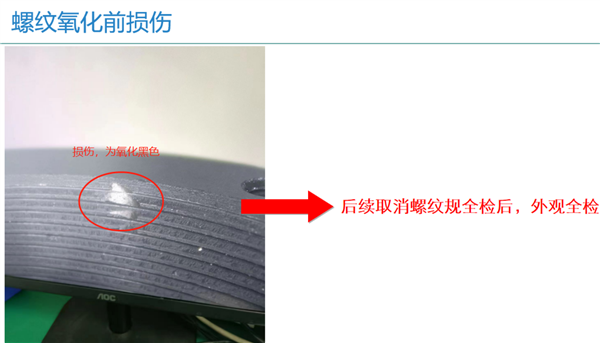
(Shows raw aluminum exposure/damage on the thread surface prior to anodizing)
📍 [Gauge Stopped by Damage / 通规止于损伤处]
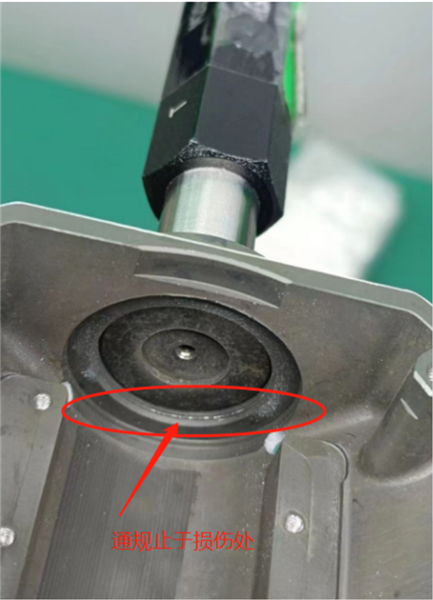
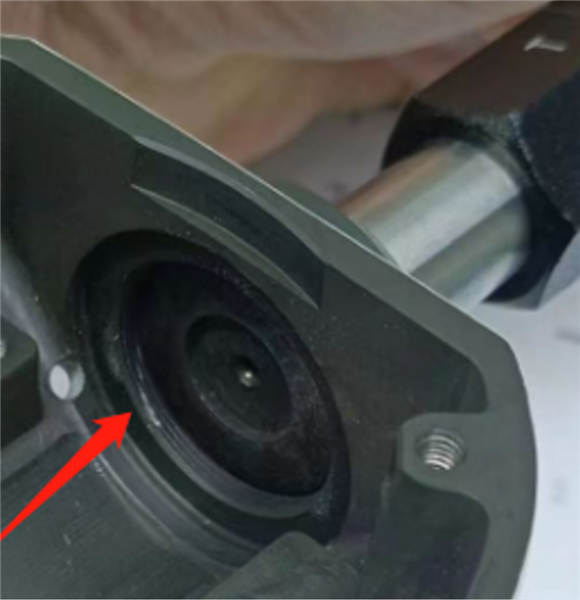
(Shows the Go-gauge binding/stopping exactly at the damaged thread area)
During the external painting process, paint splashed through two adjacent thru-holes and accumulated inside the internal thread grooves, creating interference for the Go-gauge.
📍 [Paint Overspray / 螺纹表面白色积漆]
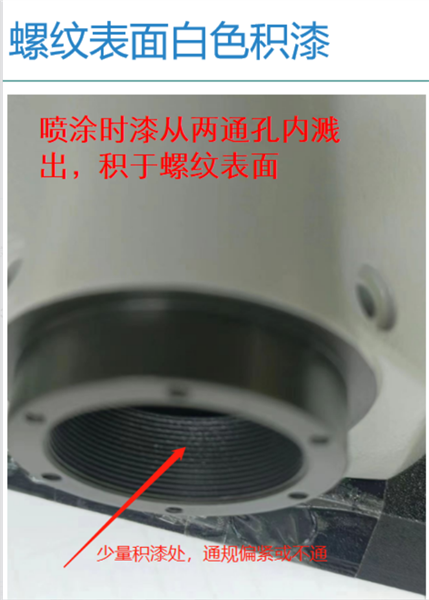
(Shows white paint accumulation in the thread grooves causing tight fit or gauge blockage)
📍 [Paint Ingress Path / 喷涂时漆从两通孔内溅出]
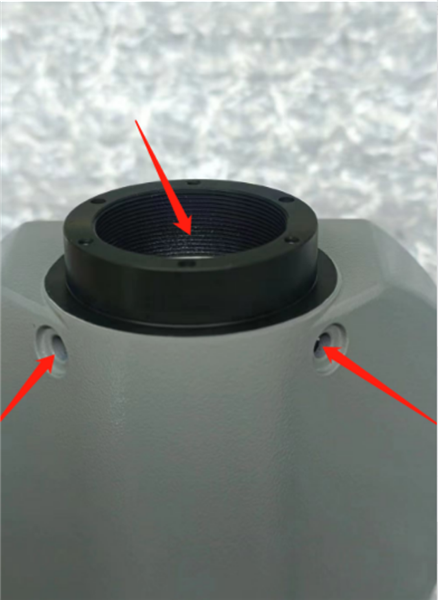
(Shows the entry point where paint splashed through adjacent thru-holes into the threaded bore)
The Standard Inspection Process (SIP) lacked explicit control for the pre-thread minor diameter 19.5+/-0.01.
Insufficient workholding rigidity led to minor thread taper toward the bottom of the hole.
📍 [ Minor Diameter Gauge Test / P4 螺纹不通分析]
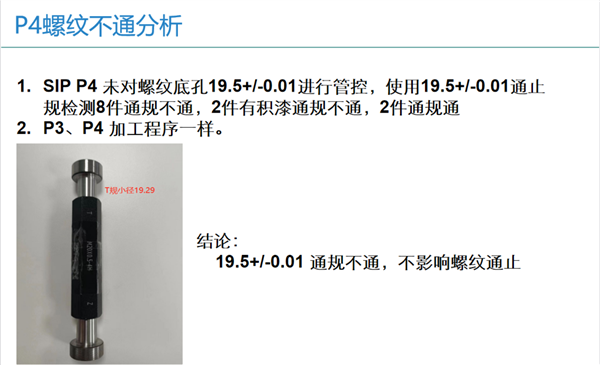
(Shows the thread gauge inspection on minor diameter 19.5+/-0.01
To eliminate these root causes, we executed targeted improvements across machining, tooling, masking design, and process routing:
📍 [Custom Gauge & Root Cause / P4螺纹不通改善]
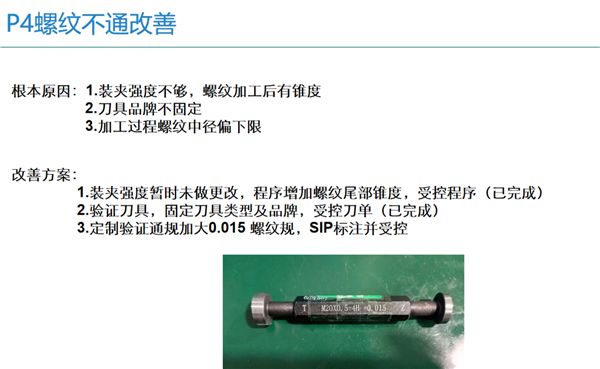
(Shows the customized +0.015 thread gauge M20X0.5-4H +0.015)
Redesigned Masking Fixture: Developed custom masking plugs/fixtures to tightly seal both the threaded bore and adjacent thru-holes during painting.
New Cleaning Protocol: Added an post-anodize ultrasonic cleaning step (70°C water, 3min) followed by water rinse, air drying, and baking at 60°C for20min.
📍 [Masking Comparison / 改善前 vs 改善后]
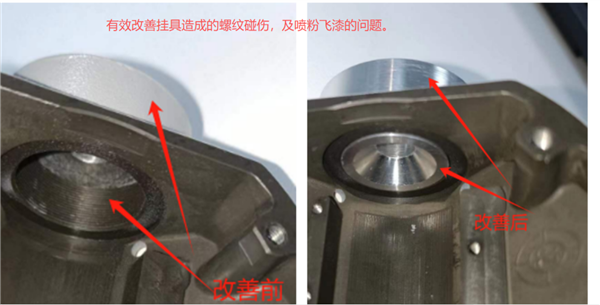
(Shows Before Improvement with paint ingress vs. After Improvement with clean, well-sealed threads)
We updated the official process flow to ensure proper sequence and protection of internal threads:
Heat Treatment->4‑Axis CNC->Lathe 1->Lathe 2->Deburring->Anodizing->Inspection->Cleaning->Internal Coating->Outsourced Painting
Inspection Strategy Update: Replaced full hard-gauge testing prior to anodizing with 100% visual inspection, shifting full thread gauge testing to post-treatment to avoid thread damage.


